Kudos Blends Ltd are the world’s leading manufacturer of technically driven baking powders and leavening agents.
They constantly invest in their manufacturing facilities ensuring that standards continually improve. As part of this drive for continuous improvement, the Mechanical Maintenance Engineer was looking to streamline the process on one of the production lines. Two areas were identified for improvement…
Positioned between the sieve outlet and holding hopper inlet, a metal detector was proving to be a bottleneck. It impeded the flow of material significantly, resulting in product piling in the centre of the hopper. This would eventually block flow, requiring the team to agitate the hopper to keep material moving. Moreover, material would also get trapped in the metal detector itself and leak into the plant, requiring clean up twice per day.
Dust emission and handling issues were a concern at the bulk bag loading station. Bags were attached to the filling head using rudimentary straps, which did not provide an effective seal.
Furthermore, bags of two differing heights were filled on the line. Metal cages were required to lift the respective bags to the correct height and keep them stable during filling. These cages were cumbersome and required two staff members, with a forklift to manoeuvre; which was challenging due to limited space in the facility. Additionally, the handling of these bags after filling was putting unnecessary pressure on the straps, causing damage that the Mechanical Maintenance Engineer was concerned may lead to a bag eventually splitting.
The brief was simple: after the maintenance team relocated the metal detector downstream to the bulk bag loading station, where it could no longer affect product flow, they would find a new way to connect the sieve to the holding hopper, whilst also looking to reduce dust levels at the bulk bag loading station.
Having already installed BFM® elsewhere around the plant, the Mechanical Maintenance Engineer enquired if we could help.
As authorised UK distributor for BFM® fitting, ProSpare’s expert BFM® team can help specify the optimum solution from the standard BFM® range, or solve unique installation challenges through the use of either “quick-release” BFM® Lipped Spigots with modular pipework, as well as Custom Fabricated Spigots.
Moving the metal detector left a gap in the process. To bridge the gap, we provided the following solution:
1. Sieve outlet – Standard welded Ø300 mm BFM® spigot
2. Connector – Ø300 mm x 400 mm. 040E Seeflex. Support ring
3. Hopper inlet – Custom Fabricated Spigot. BFM® spigot to flange, tapering from Ø300 mm to Ø200 mm, bolted directly onto hopper
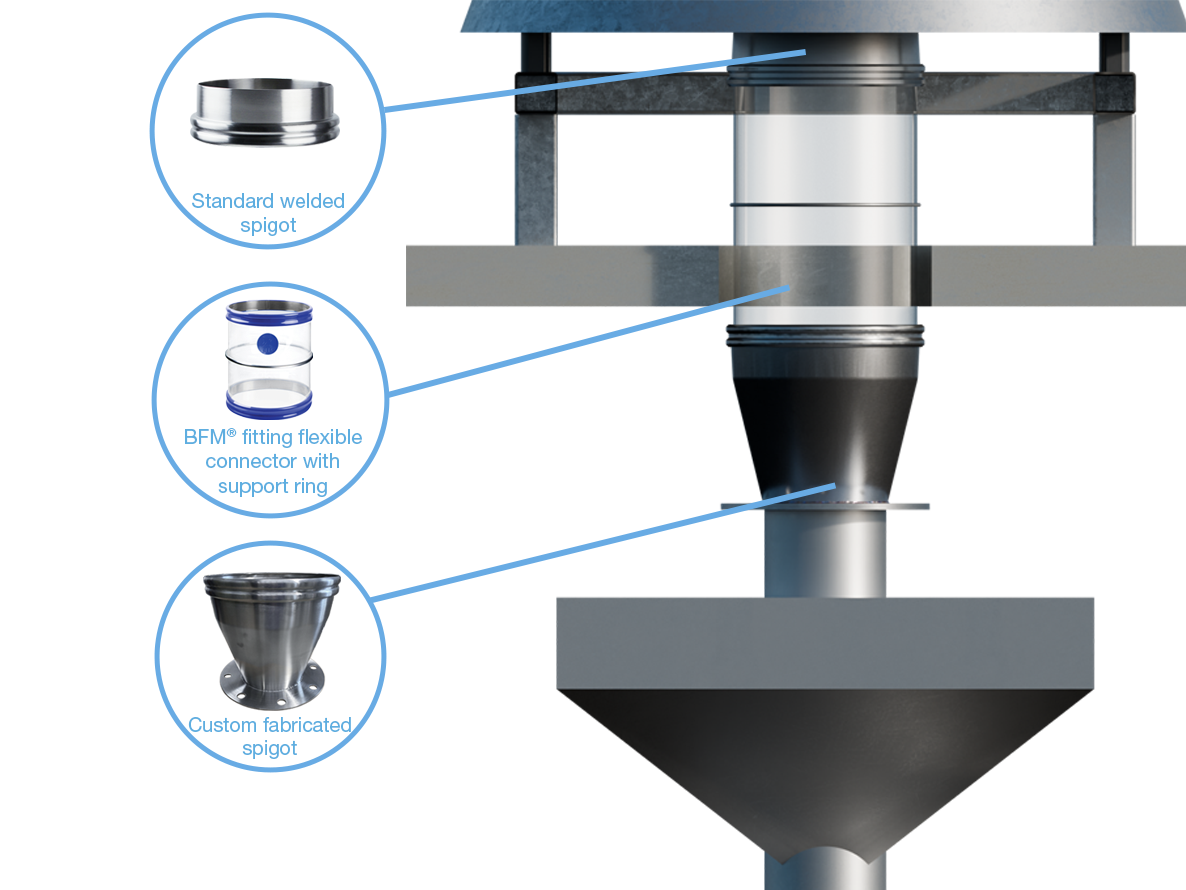 (PROJECT 1 – Redesign connection between sieve and hopper, following repositioning of metal detector)
A BFM® spigot was welded to the sieve outlet prior to moving the metal detector, so this was left untouched. A new, longer BFM® connector was ordered to snap into this spigot. These were both Ø300 mm, and with the removal of the metal detector, a new way to attach these to the Ø200 mm hopper inlet was required.
We suggested installing a Custom Fabricated Spigot with a pipework adapter that tapers from Ø300 mm to Ø200 mm. A bolted flange already existed on the hopper inlet, so we incorporated a flange into the design which enabled the maintenance team to be able to install the spigot themselves quickly and easily. This was vital, since access to the area is limited. The Mechanical Maintenance Engineer was thrilled with the design solution, stating the new spigot ‘fits like a glove.’
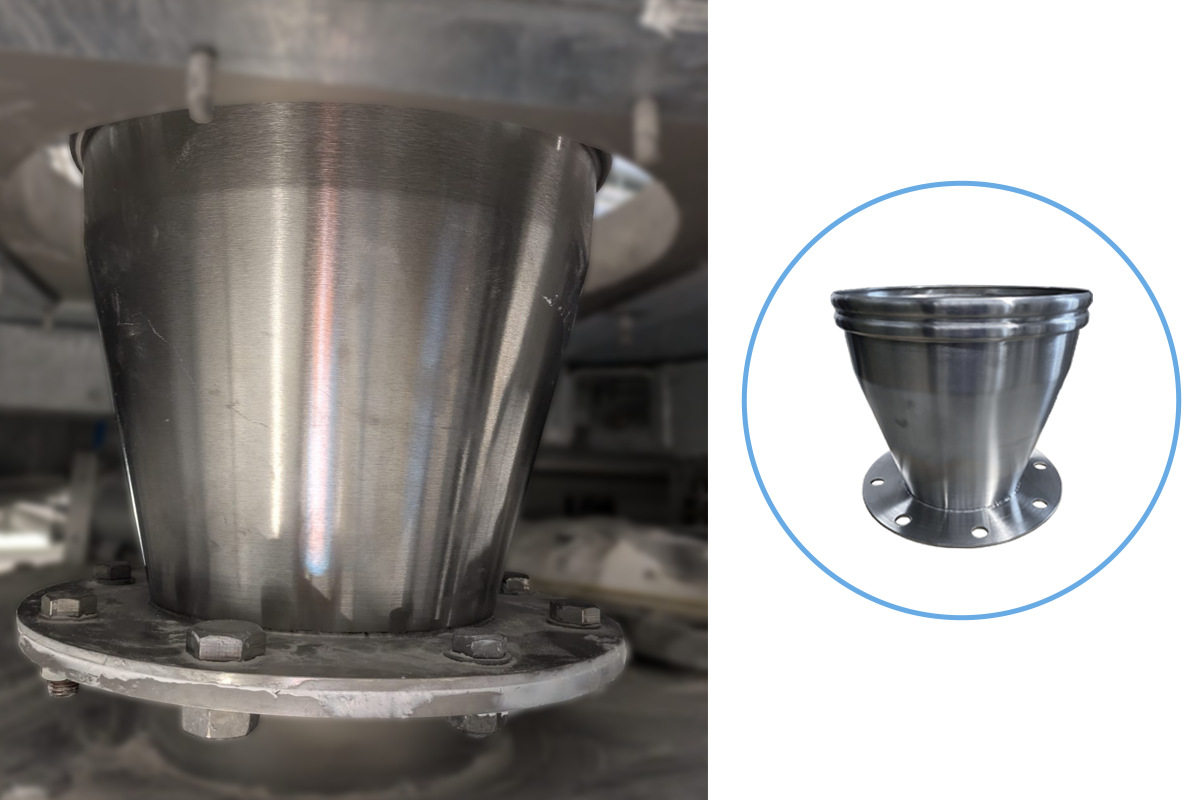 (Custom fabricated spigot. BFM® spigot to flange, tapering from Ø300 mm to Ø200 mm, bolted directly onto hopper).
The new arrangement provides unimpeded flow of material from the sieve to the hopper. Whilst production volumes vary, since installation, the Mechanical Maintenance Engineer estimates it saves around an hour each day, allowing the team to reach targets much more comfortably. Also, an estimated 70 more kilos fit into the hopper now the material is distributing evenly. Lastly, there are no longer any product leakages to clean-up daily.
In order to reduce dust levels at the bulk bag loading station, ProSpare suggested installing a BFM® Bulk Bag Loader. The BFM® Bulk Bag Loader inflates to hold the bulk bag securely in place, creating a superior seal, without the need for external straps. Since installation, the area is now much cleaner.
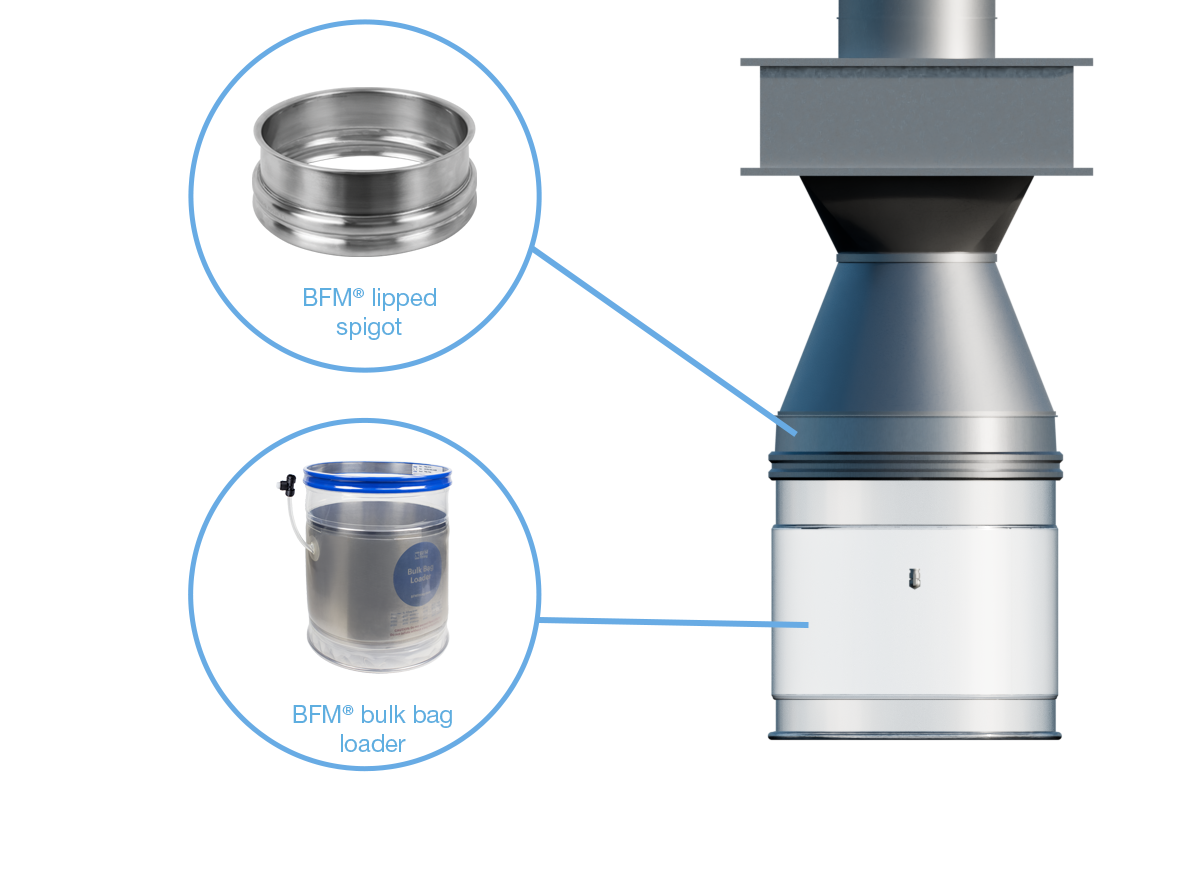 (PROJECT 2 – Reconfiguring the bulk bag loading station to reduce dust and simplify the filling process).
To cater for two different heights of bulk bag, the BFM® Bulk Bag Loader was paired with a BFM® Lipped Spigot, installed via quick-release clamps, to modular sections of pipework. This enables the team to quickly change to the desired filling height.
This, alongside the superior seal of the BFM® Bulk Bag Loader, and with a new clamping arrangement, has rendered the metal cages redundant and simplified filling operations for the production team. Loading time has been cut by 5 minutes per batch and just one member of the team is required for set-up. Additionally, simplifying the handling process has prevented damage to the straps. Removing the cages was a goal for the maintenance team who are now much happier with how the process has been streamlined thanks to BFM® fitting.
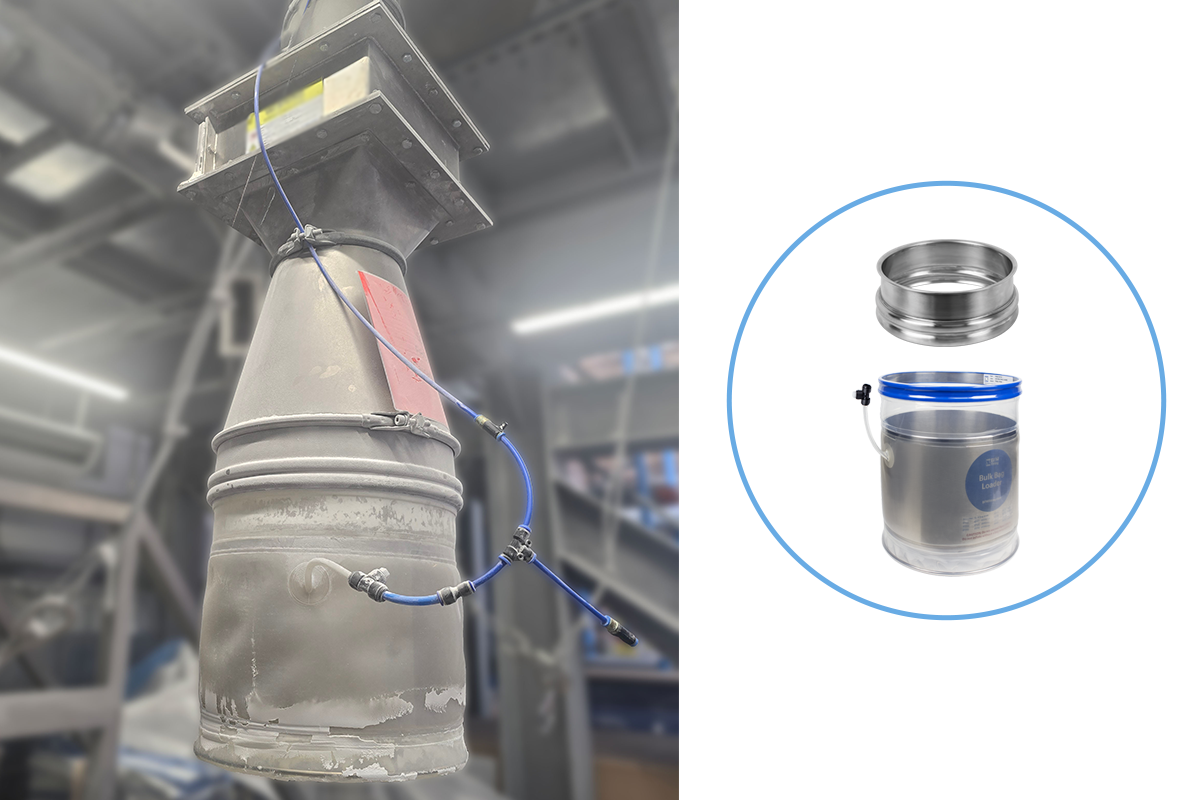 (BFM® Bulk Bag Loader with BFM® Lippped Spigot).
– Mechanical Maintenance Engineer